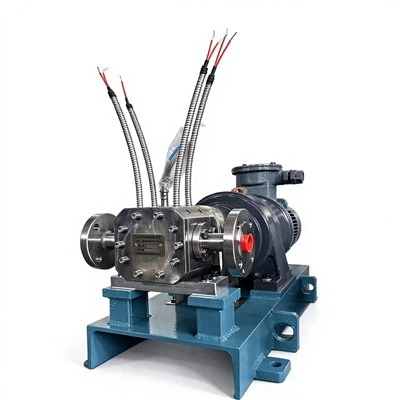
Single-acting high viscosity pumps are a crucial component in various industrial sectors, offering unique advantages for handling thick and viscous fluids. As a leading supplier of high viscosity pumps, I have witnessed firsthand the diverse application scenarios where these pumps play an indispensable role. In this blog post, I will explore some of the key application areas of single-acting high viscosity pumps and highlight the benefits they bring to each industry.
Food and Beverage Industry
In the food and beverage industry, single-acting high viscosity pumps are widely used for transferring and processing thick and sticky substances. For example, in the production of chocolate, these pumps can handle the high-viscosity chocolate mass with precision, ensuring a smooth and consistent flow during the manufacturing process. They are also employed in the transfer of honey, syrup, and other sweeteners, where maintaining the integrity of the product is essential.
One of the main advantages of single-acting high viscosity pumps in the food industry is their ability to handle shear-sensitive materials without damaging them. The gentle pumping action minimizes the risk of product degradation, preserving the flavor, texture, and quality of the food products. Additionally, these pumps are designed to meet strict hygiene standards, with easy-to-clean surfaces and materials that are resistant to corrosion and contamination.
Our High Viscosity External Gear Metering Pumps are particularly well-suited for food and beverage applications. They offer accurate metering and dosing capabilities, ensuring precise control over the amount of product being transferred. This is crucial in industries where consistency and quality are paramount.
Chemical Industry
The chemical industry deals with a wide range of high-viscosity fluids, including polymers, resins, adhesives, and lubricants. Single-acting high viscosity pumps are essential for handling these substances safely and efficiently. They can transfer chemicals from storage tanks to processing equipment, mix different components, and dispense precise amounts of chemicals for various applications.
In chemical processing, the ability of single-acting high viscosity pumps to handle high pressures and temperatures is a significant advantage. These pumps are designed to withstand the harsh conditions often encountered in chemical plants, ensuring reliable operation and long service life. They also offer excellent chemical resistance, preventing corrosion and damage to the pump components.
Our High Viscosity Metering Pump is a popular choice in the chemical industry. It provides accurate metering and dosing of high-viscosity chemicals, allowing for precise control over the production process. The pump's robust construction and advanced sealing technology ensure leak-free operation, minimizing the risk of chemical spills and environmental contamination.
Pharmaceutical Industry
In the pharmaceutical industry, single-acting high viscosity pumps are used for a variety of applications, including the transfer of viscous drugs, ointments, and creams. These pumps are designed to meet the strict quality and safety requirements of the pharmaceutical sector, ensuring the integrity and purity of the products.
One of the key challenges in pharmaceutical manufacturing is the handling of shear-sensitive drugs. Single-acting high viscosity pumps offer a gentle pumping action that minimizes shear forces, preventing damage to the active ingredients in the drugs. This is crucial for maintaining the efficacy and stability of the pharmaceutical products.


Our Magnetic Gear Pump is an ideal solution for pharmaceutical applications. It provides a hermetically sealed pumping system, eliminating the risk of leakage and contamination. The pump's magnetic coupling technology ensures a reliable and efficient transfer of high-viscosity fluids, while also reducing maintenance requirements.
Cosmetics Industry
The cosmetics industry relies on single-acting high viscosity pumps for the production and packaging of various beauty products, such as lotions, creams, gels, and lipsticks. These pumps are used to transfer and dispense the high-viscosity cosmetic formulations with precision, ensuring consistent product quality and packaging.
In cosmetics manufacturing, the ability of single-acting high viscosity pumps to handle different types of fluids, including those with varying viscosities and consistencies, is essential. They can handle both thin and thick cosmetic products, providing a versatile solution for the industry. Additionally, these pumps are designed to meet the aesthetic requirements of the cosmetics industry, with sleek and modern designs that are suitable for use in cleanroom environments.
Our high viscosity pumps offer a range of features that make them ideal for cosmetics applications. They provide accurate dosing and filling capabilities, ensuring that each product is packaged with the correct amount of cosmetic formulation. The pumps' smooth and quiet operation also makes them suitable for use in high-end cosmetic production facilities.
Construction Industry
In the construction industry, single-acting high viscosity pumps are used for a variety of applications, including the transfer of concrete, mortar, and other construction materials. These pumps are designed to handle the high viscosity and abrasive nature of these materials, ensuring efficient and reliable operation on construction sites.
One of the main advantages of single-acting high viscosity pumps in the construction industry is their ability to pump materials over long distances and at high pressures. This allows for the efficient transfer of construction materials from storage areas to the construction site, reducing the need for manual labor and increasing productivity. Additionally, these pumps are designed to withstand the harsh conditions often encountered on construction sites, such as dust, dirt, and extreme temperatures.
Our high viscosity pumps are specifically designed for construction applications, with features such as heavy-duty construction, high-pressure capabilities, and easy maintenance. They can handle a wide range of construction materials, including concrete, mortar, grout, and asphalt, providing a reliable solution for the industry.
Conclusion
Single-acting high viscosity pumps are a versatile and essential tool in various industrial sectors. Their ability to handle thick and viscous fluids with precision, reliability, and efficiency makes them a popular choice for applications where other types of pumps may not be suitable. As a supplier of high viscosity pumps, we are committed to providing our customers with the highest quality products and services.
If you are in need of a high viscosity pump for your specific application, we encourage you to contact us to discuss your requirements. Our team of experts will be happy to assist you in selecting the right pump for your needs and provide you with a competitive quote. We look forward to working with you and helping you achieve your industrial goals.
References
- "High Viscosity Pump Handbook" - A comprehensive guide to high viscosity pumps and their applications.
- "Industrial Pump Technology" - A textbook on the principles and design of industrial pumps, including high viscosity pumps.
- "Chemical Engineering Handbook" - A reference book for chemical engineers, covering a wide range of topics including fluid handling and pumping systems.