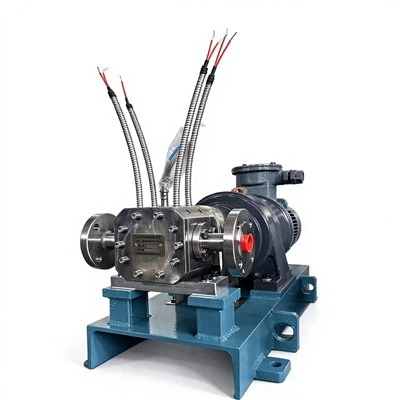
In the realm of industrial operations, chemical pumps play a pivotal role in ensuring the smooth and efficient transfer of various chemicals. The quality of these pumps can significantly impact the productivity, safety, and overall success of a chemical - handling process. As a Chemical Pump supplier, I have extensive knowledge of the market and can share insights into some of the top - quality chemical pump brands.
Grundfos
Grundfos is a well - recognized global brand in the pump industry. Their chemical pumps are engineered with high - precision technology, ensuring excellent performance and reliability. The company is committed to innovation and sustainability, which is reflected in the design of their products. Grundfos chemical pumps are known for their energy - efficient operation, which can lead to significant cost savings over time. They use advanced materials in their construction, such as corrosion - resistant alloys and high - grade plastics, making them suitable for handling a wide range of aggressive chemicals. For instance, their centrifugal chemical pumps are designed to handle both low - viscosity and high - viscosity chemicals with ease. These pumps can be used in applications such as chemical processing plants, water treatment facilities, and pharmaceutical manufacturing. The brand also offers comprehensive after - sales support, including maintenance services and spare parts availability, which gives customers peace of mind when investing in their products.
Sulzer
Sulzer is another leading brand in the field of chemical pumps. With a long - standing history of excellence, Sulzer has developed a reputation for manufacturing high - quality pumps that can withstand the most demanding industrial environments. Their chemical pumps are designed with state - of - the - art hydraulic technology, which provides high efficiency and low NPSH (Net Positive Suction Head) requirements. This means that the pumps can operate effectively even when dealing with difficult suction conditions. Sulzer offers a wide range of pump types, including centrifugal pumps, diaphragm pumps, and piston pumps, each tailored to specific chemical - handling needs. For example, their diaphragm pumps are ideal for handling abrasive and viscous chemicals, as they can provide a pulsation - free flow. The brand's commitment to quality is evident in their strict manufacturing processes, which adhere to international standards. Sulzer also invests heavily in research and development to continuously improve their product offerings and meet the evolving needs of the chemical industry.
Flowserve
Flowserve is a global provider of flow control products and services, and their chemical pumps are among the best in the market. Their pumps are designed to handle a diverse range of chemicals, from corrosive acids to high - temperature fluids. Flowserve uses advanced sealing technologies in their pumps, which prevent leakage and ensure the safety of the operating environment. Their magnetic drive pumps, for example, eliminate the need for traditional shaft seals, reducing the risk of chemical spills and improving overall reliability. The company also offers a variety of customization options, allowing customers to tailor the pumps to their specific application requirements. Flowserve has a vast network of service centers around the world, providing prompt and efficient support to customers. This global presence ensures that customers can get the help they need, no matter where they are located.
KSB
KSB is a well - established brand that has been manufacturing pumps for over a century. Their chemical pumps are known for their robust construction and long - service life. KSB pumps are designed to meet the highest safety and quality standards, making them a reliable choice for chemical - handling applications. The company offers a comprehensive range of pump solutions, including horizontal and vertical centrifugal pumps, as well as submersible pumps. Their pumps are suitable for use in industries such as petrochemicals, mining, and food and beverage. KSB also focuses on energy efficiency, and many of their pumps are designed to reduce power consumption while maintaining high performance. The brand's commitment to innovation is evident in their development of new pump technologies, such as intelligent pump systems that can optimize performance based on real - time operating conditions.
Iwaki
Iwaki is a Japanese brand that specializes in the production of chemical pumps. Their pumps are renowned for their high - quality and precision engineering. Iwaki offers a wide range of chemical pumps, including magnetic drive pumps, centrifugal pumps, and peristaltic pumps. Their magnetic drive pumps are particularly popular in the chemical industry due to their leak - free design and excellent chemical resistance. These pumps are suitable for handling a variety of chemicals, including solvents, acids, and alkalis. Iwaki also places a strong emphasis on environmental protection, and their pumps are designed to minimize energy consumption and reduce waste. The company's products are used in various industries, such as electronics manufacturing, semiconductor production, and water treatment.
Our Company's Chemical Pumps
As a Chemical Pump supplier, we are proud to offer a range of high - quality chemical pumps that can meet the diverse needs of our customers. Our pumps are designed and manufactured with the latest technology and the highest quality materials. We understand the importance of reliability and efficiency in chemical - handling processes, and our pumps are built to deliver outstanding performance.


One of our featured products is the Novolak Resin Electric Heating Gear Metering Pump. This pump is specifically designed for handling novolak resin, which requires precise metering and heating. The electric heating system ensures that the resin remains at the optimal temperature during the pumping process, preventing solidification and ensuring smooth operation.
Another product is the Electric Heat System For Convey Asphalt Gear Metering Pump. This pump is ideal for conveying asphalt, a high - viscosity material that requires a reliable and efficient pumping solution. The electric heat system helps to maintain the fluidity of the asphalt, allowing for accurate metering and smooth transfer.
You can also explore our general Chemical Pump range, which includes a variety of pump types suitable for different chemical - handling applications. Our pumps are available in different sizes and configurations to meet the specific requirements of your project.
Contact Us for Procurement
If you are in the market for high - quality chemical pumps, we invite you to contact us for procurement. Our team of experts is ready to assist you in selecting the right pump for your needs. We can provide detailed product information, technical support, and competitive pricing. Whether you are a small - scale chemical manufacturer or a large - scale industrial enterprise, we have the solutions to meet your chemical - handling requirements. Don't hesitate to reach out to us to start a fruitful business relationship.
References
- Chemical Pumps Handbook, McGraw - Hill Professional
- Industrial Pump Technology, Wiley
- Pump User's Handbook: Life Extension, McGraw - Hill Professional